Continuous automated equipment designed for high-density composite siding, cellular lightweight block manufacturing, and sustainable exterior thermal envelopes across Dakahlia Governorate.
Analyzing the industrial acceleration of Dakahlia Governorate, the logistical nexus of New Mansoura, and the urgent demand for energy-saving, flame-retardant exterior building envelopes.
With the rapid deployment of New Mansoura City along the Mediterranean coast, regional building standards have shifted radically toward prefabricated thermal envelope systems. Covering over 2,000 feddans in phase one, the smart city initiative mandates strict adherence to the Egyptian Energy Efficiency Code for Buildings (EEEC), penalizing thermal bridging and heavy wet construction.
Mansoura and nearby industrial centers such as Gamasa Industrial Zone and Sandub enjoy direct logistical connectivity to Damietta Port (approx. 65 km) and Alexandria Port. This positioning offers localized manufacturing plants an unmatched supply advantage for imported Aluzinc (Al-Zn coated steel) coil, fluorocarbon (PVDF) finishes, and rigid polyurethane precursors.
Egyptian currency realignments and import tariffs have made finished architectural facade panels prohibitively expensive for private real estate developers. Establishing an in-situ embossed metal composite panel production line in Mansoura enables localized production at 40-55% lower landed costs while securing robust domestic margins.
Engineered for high-volume structural durability, multi-texture architectural rolling, and automated chemical metering tailored to the climatic specifics of the Mediterranean Delta basin.
Embossed metal composite exterior panels—frequently designated as polyurethane metal carved thermal insulation boards—represent the zenith of modern building envelope technology. The panel structure integrates three fundamental material layers: a 0.27mm–0.50mm fluorocarbon/high-weatherability polyester-coated Al-Zn alloy steel sheet (surface layer), a high-pressure injected rigid polyurethane (PUR) or polyisocyanurate (PIR) closed-cell core (intermediate thermal layer), and an aluminum foil coated fiber cloth or glass fiber fabric (backing moisture barrier).
For industrial plants operating in Mansoura and Dakahlia, environmental conditions introduce distinct engineering challenges: Mediterranean humidity from Gamasa and the coastal axis, high summer ambient temperatures reaching 42°C, and soil-borne salinity. Our turnkey production lines incorporate hardened alloy embossing rollers with chrome-plated mirror finishes (HRC 60–62), precision temperature-controlled preheating tunnels, and high-pressure pentane/HCFC-free polyurethane injection rigs to eliminate delamination, bubbling, and dimensional warpage.
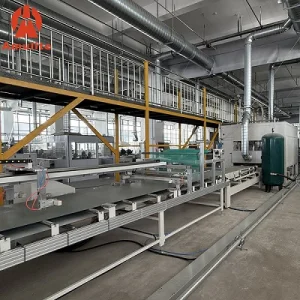
Dual-mandrel pneumatic hydraulic uncoiler with automatic tension loop control and PE protective film lamination station to preserve exterior PVDF coil finishes.
Heavy-duty dual-roller embossing press with hydraulic micro-gap adjustment, imprinting deep textures (brick, marble, timber grain, stucco, stone mosaic).
18 to 24-station precision roll-forming unit shaping male/female locking joints (tongue and groove) with hidden fastener channels to prevent capillary water ingress.
Infrared electrical preheating chamber ensuring coil substrate temperature reaches 45°C–55°C, optimizing polyurethane adhesion and uniform chemical nucleation.
High-pressure dynamic mixing head driven by high-accuracy axial piston metering pumps, dispensing uniform PIR/PUR foam across a dual-axis oscillating carriage.
24-meter to 36-meter high-rigidity continuous caterpillar press with circulating hot-air PID heating, maintaining exact panel thickness and foam curing density.
Servo-driven hydraulic traveling circular saw with carbide tips, tracking line speeds up to 12 m/min with ±1.0mm cutting accuracy and zero edge-burr.
Modular cooling conveyor line allowing complete polymer crystallization, integrated with vacuum-suction stacker and orbital shrink packaging.
| Technical Parameter | Standard Performance Range | Amulite High-Speed Mansoura Spec | Compliance / Verification Method |
|---|---|---|---|
| Line Operational Speed | 4.0 – 8.0 m/min | 6.0 – 12.0 m/min (Continuously Variable) | Siemens S7-1500 PLC Synchronized Closed-Loop |
| Panel Width Range | 350 mm – 450 mm (standard 380 mm) | 380 mm / 400 mm / 450 mm Architectural Standard | Adjustable Tooling & Modular Roll Stations |
| Panel Finished Thickness | 16.0 mm – 20.0 mm | 16.0 mm – 50.0 mm (Insulated Commercial Grade) | Hydraulic Synchronous Caterpillar Gap Control |
| Steel Coil Thickness Compatibility | 0.25 mm – 0.35 mm | 0.27 mm – 0.50 mm (Alu-Zinc 100g/m² – 150g/m²) | EN 10346 / ASTM A792M Structural Compliance |
| Core Foam Density | 38 – 42 kg/m³ | 42 – 48 kg/m³ (High Mechanical Compressive Index) | ISO 845 / ASTM D1622 Closed-Cell Verification |
| Reaction to Fire Index | B2 Class (Combustible) | B1 / Class 1 / Class A Flame-Retardant PIR Formulation | EN 13501-1 / ASTM E84 Tunnel Flame Index ≤ 25 |
| Installed Total Power Rating | 110 kW – 160 kW | 135 kW (Equipped with Regenerative Inverters) | 380V / 50Hz, 3-Phase Egyptian Grid Optimized |
Overcoming operational vulnerabilities: Chemical storage dynamics, power fluctuations, and adherence to Egyptian fire safety codes.
Delta summers subject chemical feedstocks to boiling points and premature crystallization. Our plant packages integrate automatic chiller units, heated jacketed storage tanks (20°C–24°C stabilization), and closed-loop nitrogen blankets to shield raw chemicals from moisture contamination and guarantee stable foam density throughout high-humidity spells.
Industrial sub-grids in Dakahlia can experience sudden load fluctuations. We equip every production line with centralized voltage stabilization units, transient voltage surge suppressors (TVSS), and industrial harmonic filters, ensuring steady 380V/50Hz operation and protecting precision Beckhoff and Siemens servo drives from unexpected factory blackouts.
The Egyptian Building Code mandates stringent fire propagation resistance for high-rise commercial facades in New Mansoura. Our specialized chemical dosing systems accommodate high-index polyisocyanurate (PIR index > 250) formulations with organophosphorus flame retardants, generating non-dripping carbonized char barriers during open-flame exposure.
Purchasing an overseas production line represents a multi-million-pound capital expenditure. Amulite Group eliminates execution risk through our proven Turnkey Deployment Protocol. From soil load bearing engineering drawings to mechanical leveling, electrical tie-in, test formulation runs using localized Egyptian chemical suppliers, and bilingual (English/Arabic) machine operator training, our senior engineering teams supervise every project on-site in Mansoura until target throughput and quality standards are fully reached.
Pioneering advancements in low-carbon foaming agents, AI automated inspection, and integrated Building Integrated Photovoltaic (BIPV) composite facades.
As international environmental standards tighten, Egyptian exporters targeting Europe or the GCC require green certifications. Our lines are pre-configured for safe cyclopentane foaming, incorporating explosion-proof EX-rated motor enclosures, catalytic gas leak detection sensors, and automated purge cycles to achieve near-zero Global Warming Potential (GWP < 1).
Continuous online machine-vision scanners mounted immediately post-cooling monitor emboss depth conformity, coating micro-scratches, and tongue-and-groove dimensional variance at 12 m/min. Defective boards are flagged and tracked automatically via ink-jet barcode tagging without halting line feed speeds.
The frontier of Egyptian building envelopes combines thermal metal carved cladding with thin-film solar cell integration. Our development labs are validating roll-forming lines capable of embedding wiring conduits and junction pockets within the insulated PIR matrix, transforming exterior building panels into clean electricity generation assets.
Explore auxiliary plants, EPS sandwich wall panel machinery, XPS continuous foam lines, and automated crushing units operating across global reference facilities.
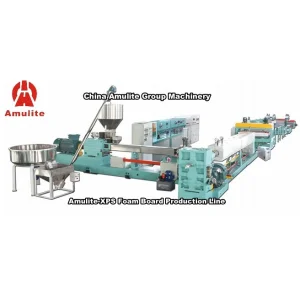
Direct technical and commercial clarifications regarding shipping logistics, workshop space requirements, raw material sourcing, and operational payback periods.
A standard continuous embossed metal panel production line with a 24-meter double caterpillar conveyor requires a linear workshop length of at least 85 to 100 meters, a minimum clear span width of 18 meters, and a minimum eave clearance of 6.0 meters to comfortably accommodate raw coil staging, chemical storage tanks, caterpillar assembly, flying saw run-out, and auto packaging stations.
Yes. Leading Egyptian steel suppliers (e.g., Ezz Steel, Kandil Steel) produce compatible galvanized and Aluzinc steel coils (0.27mm–0.40mm with exterior grade paints). For chemical precursors, major global petrochemical suppliers maintain bulk distribution hubs in Alexandria and 6th of October City, supplying MDI and formulated polyol polyether blends directly to factories in Dakahlia.
Manufacturing lead time ranges from 90 to 120 days depending on roller pattern customization. Machinery is containerized into 40ft High Cube containers and shipped from Tianjin or Qingdao Port directly to Damietta Port (only 65 km north of Mansoura) or Alexandria Port. Ocean freight to Damietta typically takes 25 to 35 days, facilitating rapid customs clearing and inland drayage.
The front skin utilizes 55% Aluminum-Zinc alloy coated steel (Galvalume) sealed with fluorocarbon (PVDF) or high-durability polyester (HDP) paint systems, passing 1,000+ hours of continuous salt spray testing (ASTM B117). The rigid PUR/PIR core achieves a closed-cell ratio over 95%, completely preventing moisture penetration and rotting common in traditional masonry wall systems.
Given the continuous expansion of New Mansoura, coastal villa communities, and renovation projects across the Delta, local wholesale demand for carved insulation siding commands substantial premiums. Based on a single 8-hour shift operating at 60% capacity (approx. 500,000 m²/year), payback on mechanical capital equipment typically materializes within 14 to 22 months of steady production.
We deploy senior mechanical engineers, PLC software specialists, and chemical foaming technicians to your factory site in Egypt. In addition to commissioning the line, we provide complete mechanical schematics, standard wear-part spares for 2 years of continuous operation, and 24/7 remote IoT VPN diagnostics directly linked to our control engineering labs.
Connect with China Amulite Group’s process engineering specialists. Receive detailed foundation layout drawings, utility load requirements, full line equipment pricing, and localized raw material formulation guides customized for the Egyptian construction market.